Colour matching across components: Pantone, masterbatch and lot tolerance
Matching a cap to a bottle is not the same problem as matching a print to a label. Where colour drift comes from, how to set a tolerance, and why the second production run is the one that matters.
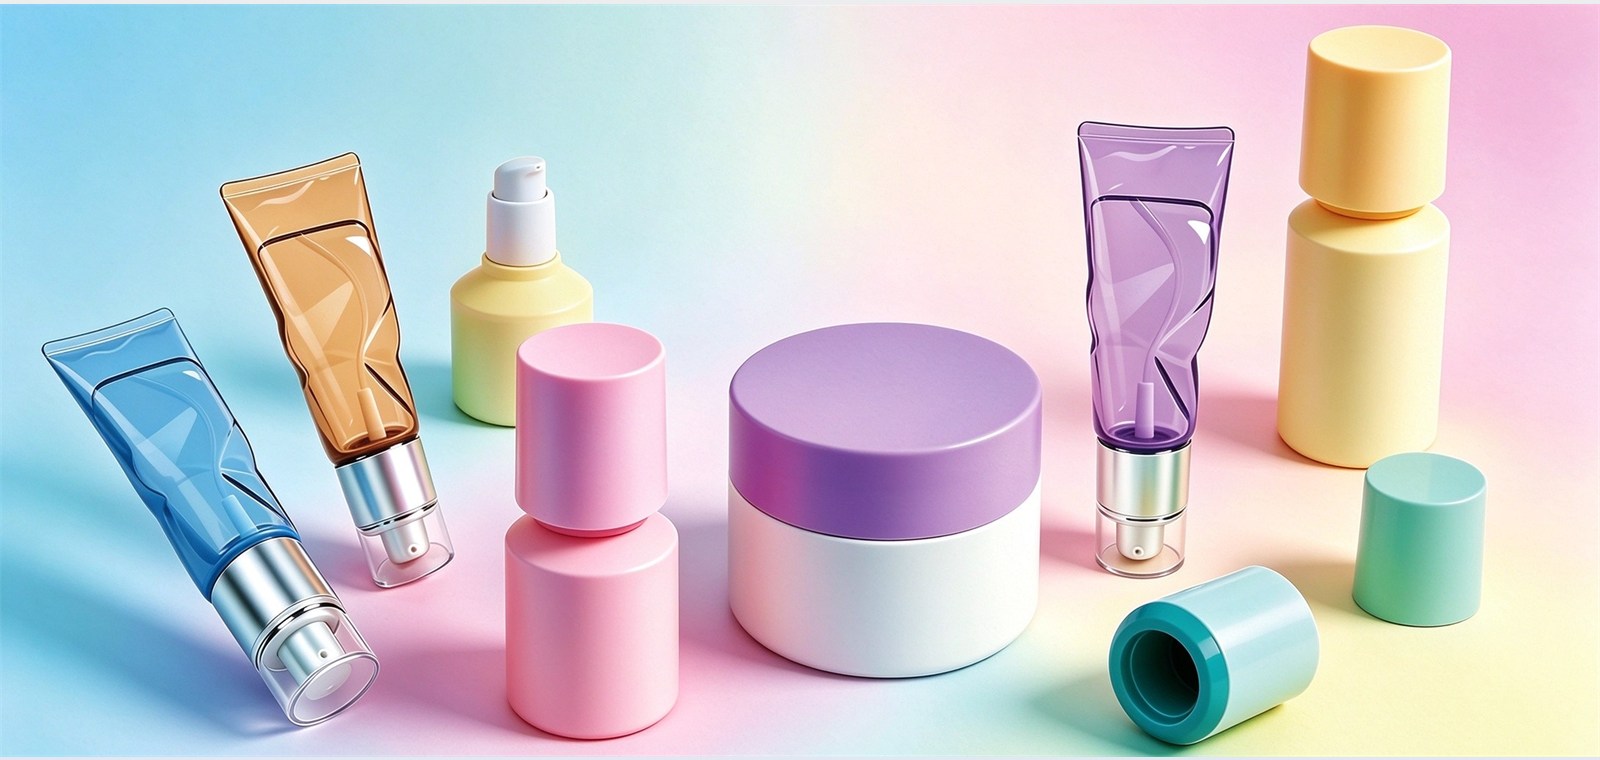
A launch usually starts with one Pantone chip and a sentence: make everything this colour. Then the cap arrives slightly cooler than the bottle, the tube is a shade lighter than the jar, and the label printer says their ink cannot hit it on that stock.
Colour matching across components is a series of separate problems that look like one.
Where drift actually comes from
Three things move colour in moulded parts, and only one of them is the pigment.
The first is substrate. The same masterbatch in PET and in HDPE does not read the same: PET is glossy and clear-based, HDPE is opaque and slightly waxy, and a colour measured on one is not transferable to the other.
The second is wall thickness. A thick section holds more pigment per unit area and reads darker than a thin one, which is why a tube shoulder can differ from its body even when both come from the same batch.
The third is process. Injection, extrusion and blow moulding shear the melt differently, and some pigments are shear-sensitive.
Masterbatch is not paint
Masterbatch colours the resin from the inside; the part is that colour all the way through, including any scuff. Painting and metallising sit on the surface and can be matched to a chip more exactly, but they chip, and they add a process step to the lead time.
For a family where a cap must match a bottle, our usual recommendation is masterbatch on both, matched from the same pigment lot, rather than masterbatch on one and paint on the other. Two processes never match as closely as one process run twice.
What a tolerance number means
Colour difference is measured as Delta E, a single number describing how far a sample sits from the standard. On moulded cosmetic packaging, a working tolerance is usually Delta E 2 or better for parts that sit next to each other in the same pack, and looser for parts that are never seen together.
Ask for the tolerance in the quotation rather than after the first reject. A supplier who promises "exact match" is telling you they have not measured it.
Approving a standard
Approve a physical standard, not a screen. A Pantone chip is a starting point; the approved reference should be a moulded plaque or an actual production part, signed and dated, with the resin and the masterbatch lot recorded.
Keep two: one for the supplier, one for your own archive. When a dispute comes up two years later, the archived part settles it in a minute.
Why the second run matters more than the first
The first production run is usually matched by eye with extra care because everyone is watching. The second run, six months later, is where lot-to-lot variation shows up.
Two things control it: specifying the masterbatch supplier and grade in the purchase order, and asking for a retained sample from each lot. If the colour is critical to the brand, the retained samples are worth more than the certificate.
A practical sequence
- Choose the colour on the final substrate, not on paper.
- Approve a moulded plaque, not a printed chip.
- Agree the Delta E tolerance in writing.
- Record resin grade and masterbatch lot on the approved standard.
- Keep a retained sample per production lot.
Do those five and the colour conversation ends at sampling instead of restarting at every reorder.
Specifying this for a real product? Send the drawing or a reference sample.